In pharmaceutical production, compressed gases—including compressed air, nitrogen, and carbon dioxide—are no longer viewed as simple “utility sources.” Instead, they act as critical process materials that come into direct contact with drug solutions, powders, primary packaging materials, and sterile working surfaces. If compressed gas carries microorganisms into critical production areas, it poses a risk not just of single-point deviations or localized cleanliness issues, but of whole-batch product contamination.
Compared to routine airborne viable particle monitoring (settle plates and active air sampling), microbial testing of compressed gases has historically lacked a unified, standardized approach. This article systematically reviews mainstream regulatory standards, recommended testing frequencies, and sample volumes, while analyzing the principles, pros, cons, and application scenarios of mainstream testing methodologies to provide a reference framework for pharmaceutical enterprises.
1. Standard and Regulatory Requirements
The microbial assessment of compressed gases is not governed by a single standard, but rather by a multi-layered framework combining GMP guidelines, pharmacopoeias, and compendial standards.
1.1 GMP Regulatory Landscape
EU GMP Annex 1 and China GMP Annex 1 (2026 Draft Revision) explicitly incorporate compressed gases into the validation and routine monitoring scope of utility systems. They require that compressed gases coming into direct contact with products must have microbial and particle quality “equal to or better than the air quality of the environment in which they are used.” Compressed gases must be regularly monitored for dew point, oil content, suspended particles, and microorganisms.
FDA Guideline on Sterile Drug Products Produced by Aseptic Processing (2004) similarly dictates that compressed gases should maintain appropriate purity (e.g., oil-free), and the filtered microbial and particle quality should be equal to or better than the air environment into which the gas is introduced.
1.2 Limit Requirements
Regulatory frameworks rarely dictate absolute microbial limits for compressed gases directly; instead, they rely on the principle of being “equal to or better than the surrounding environment.” Enterprises must establish internal control standards based on the cleanliness grade of the point-of-use, referencing corresponding environmental viable count limits.
Key Principle: Compressed gases directly contacting sterile products must meet sterility requirements (SAL10-6), and their microbial monitoring limits should be no lower than Grade A environmental viable particle standards (<1CFU/m3). Non-direct contact process gases can be assigned limits corresponding to their use-point environmental classification.
2. Recommended Testing Frequency and Sample Volume
2.1 Testing Frequency
Testing frequencies should be determined via risk assessment. Core considerations include: whether the gas directly contacts the product, the cleanliness grade of the use-point, system design and sterilizing filter configuration, and historical monitoring trend data. Industry-standard frequency recommendations are outlined below:
| Point-of-Use Environment Grade |
Recommended Monitoring Frequency |
Description |
| Grade A / Critical Zone |
At least 1x per production shift |
Key gas usage points directly contacting sterile products; recommended to run concurrently during filling and other critical operations. |
| Grade B / Support Zone |
1x daily |
Sterile production support areas, covering daily production cycles. |
| Grade C |
1x weekly |
Non-sterile production or controlled cleanliness areas. |
| Grade D |
1x monthly |
General clean areas; can be adjusted in combination with system revalidation cycles. |
Additionally, monitoring frequencies should be increased under the following circumstances: after system maintenance or replacement of sterilizing filter elements; when restarting after a long shutdown; upon occurrence of deviations or out-of-specification (OOS) results; or when process changes might impact gas quality.
2.2 Recommended Sample Volume
It is recommended to use 1 cubic meter (1000L) of gas as the standard sample volume, with results reported in CFU/m3. This volume is established based on statistical detection requirements under low microbial concentrations—since expected microbial concentrations in Grade A zones are extremely low, insufficient sampling volumes can lead to false negatives.
In practice, if site conditions prevent reaching 1000L, the sample volume may be appropriately reduced, provided that the limit of detection (LOD) under that volume is confirmed via risk assessment and documented. For critical gas-use points with high sterility requirements, large-volume sampling is strongly recommended to maximize detection sensitivity.
Note: Before sampling, purge the pipeline for 5 to 10 minutes to clear stagnant gas and ensure a representative sample is collected. All sampling apparatus coming into contact with the gas must be sterilized, and the sampling ports disinfected with sterile sanitizer.
3. Detailed Analysis of Six Mainstream Testing Methods
The core challenge in compressed gas microbial testing lies in the fact that when high-pressure gas expands suddenly to atmospheric pressure, the shear force generated by rapid expansion can damage microorganisms, leading to poor recovery rates or irreproducible conditions.
| Method |
Core Principle |
Sampling Quantitation |
Microbial Recovery Rate |
| Pressure-Maintained Impaction |
Impaction under pressurized conditions |
Strong (CFU/m3) |
High |
| Pressure-Reduction Method |
Impaction after pressure reduction |
Strong (CFU/m3) |
Low |
| Direct Agar Plate Sweep |
Direct blowing toward agar |
Weak (cannot quantify accurately) |
Low and high fluctuation |
| Air Sampler Blow Sweep |
Sweeping and impaction |
Strong (CFU/m3) |
Low |
| Liquid Recovery Method |
Bubbling through liquid capture |
Strong (combined with membrane filtration) |
High fluctuation |
| Membrane Filtration Method |
Physical trapping via microporous membrane |
Strong (CFU/m3) |
Relatively High |
Six commonly used methods approach these challenges through different technical pathways:
3.1 Pressure-Maintained Impaction
Principle: Maintains constant pressure while gas passes through a perforated plate directly onto an agar surface in a pressurized environment, followed by normal pressure restoration and incubation.
Advantages: Avoids shear stress damage from sudden pressure drops, yielding higher survival and recovery rates; superior physical particle capture under high pressure.
3.2 Pressure-Reduction Method
Principle: Reduces gas to normal pressure via a valve, then accelerates airflow through a modified air sampler so microbes impact the agar surface by inertia.
Advantages: Simple operation using standard atmospheric equipment.
Limitations: Complex valve structures and deceleration trap many microorganisms inside, resulting in low recovery.
3.3 Direct Agar Plate Sweep
Principle: After simple pressure reduction, gas is blown directly at a set distance and angle onto an agar plate, relying on natural settling and inertial impaction.
Advantages: Easy operation, equipment-free, and extremely low cost.
Limitations: Hard to measure sampling volume accurately (qualitative/semi-quantitative only); uncontrollable flow velocity causes high recovery fluctuations and poor reproducibility; high-speed air risks microbial damage and false negatives.
3.4 Air Sampler Blow Sweep
Principle: Compressed gas is blown across a target zone while a conventional viable air sampler is placed downstream, adapting an environmental sampler for compressed gas.
Advantages: High equipment penetration rate and low retrofitting costs.
Limitations: Flow direction discrepancies cause many particles and microbes to separate after redirection, leading to low recovery.
3.5 Liquid Recovery Method
Principle: Gas is channeled into liquid media or sterile buffer, bubbling through the liquid to capture microbes before filtration or inoculation and incubation.
Advantages: Simple equipment and lower cost.
Limitations: Bubble capture efficiency is affected by flow rate, bubble size, and liquid properties, making recovery unstable and hard to validate.
3.6 Membrane Filtration Method
Principle: Quantified gas passes through a 0.45μm (or 0.22μm) microporous membrane to physically retain microbes, which are then placed on solid media for colony counting.
Advantages: Handles large gas volumes with high sensitivity; clear physical retention mechanism and relatively simple operation.
Limitations: Filtration efficiency is limited over long cycles; high-pressure blast can damage membranes or allow penetration; risk of cell desiccation and death on dry membranes.
Through the comparison of these 6 methods, the Pressure-Maintained Impaction method successfully resolves challenges including shear-force damage, sample volume control, test condition reproducibility, and microbial recovery, making it the preferred method for compressed gas microbial testing.
Conclusion
As regulatory scrutiny intensifies worldwide, robust microbial monitoring of compressed gases is a vital compliance and quality-assurance safeguard for pharmaceutical companies.
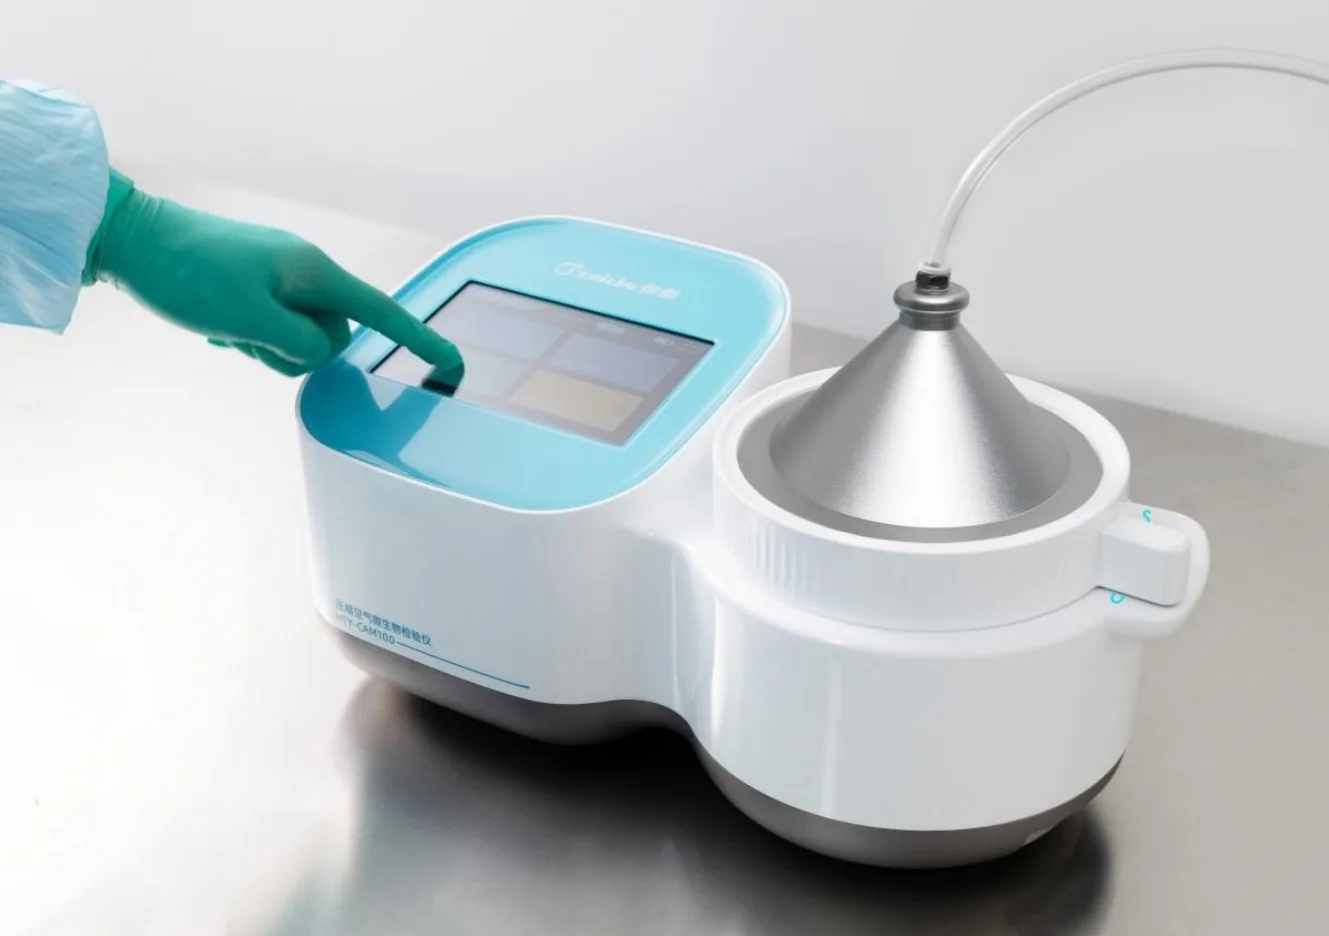
Actively contributing to industry advancement, Tailin introduced the HTY-CAM100 Compressed Air Microbial Sampler, a state-of-the-art Compressed Air Microbial Sampler utilizing the advanced pressure-maintaining impact method to achieve top-tier recovery rates. Equipped with security permission management, data export, and filtered exhaust capabilities, the HTY-CAM100 successfully resolves industry pain points and empowers pharmaceutical manufacturers to strengthen quality control and risk management.
For more information or to explore partnership opportunities, please visit our website or contact us at phone: +86 571 8658 9087, email: marketing@tailingood.com. Stay connected with Tailin through our social media channels on Facebook, YouTube, LinkedIn and Instagram to witness our ongoing journey toward excellence and innovation.